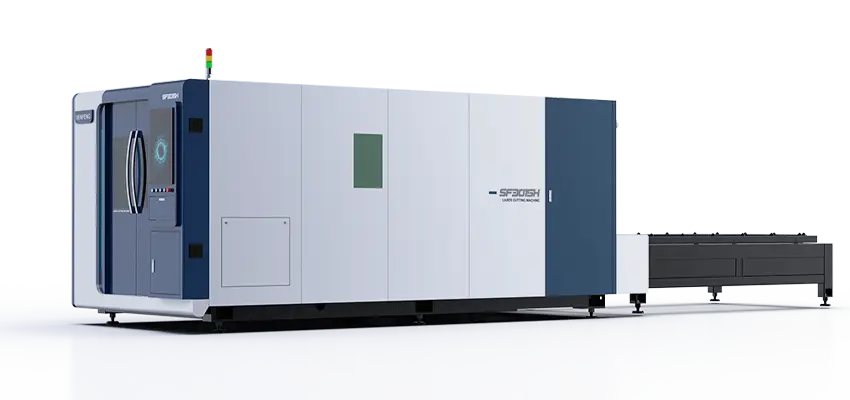
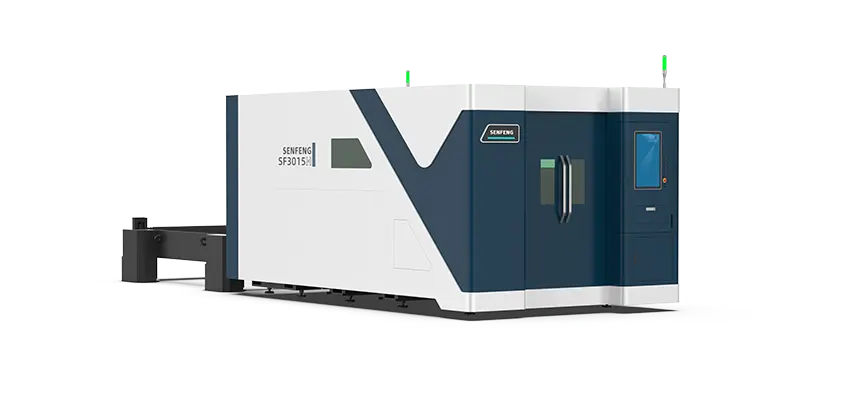
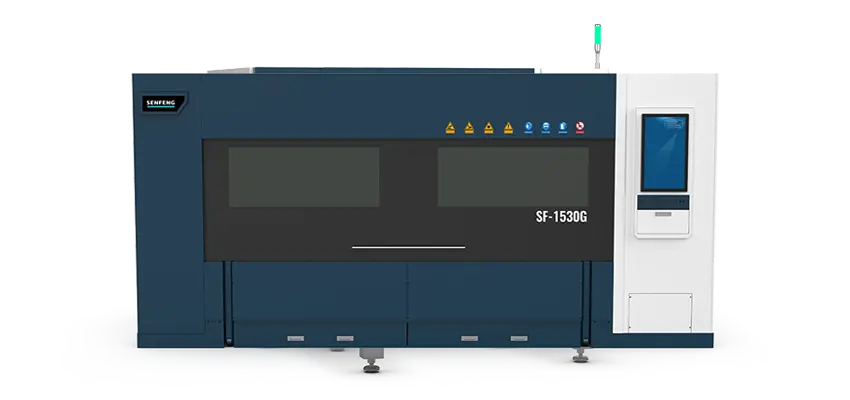
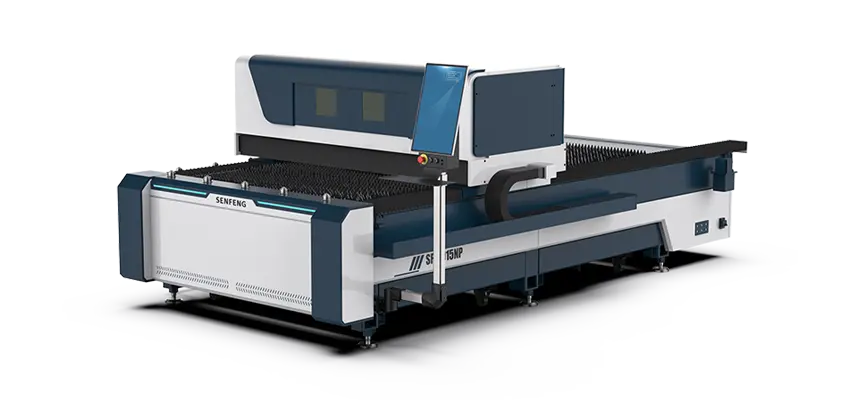
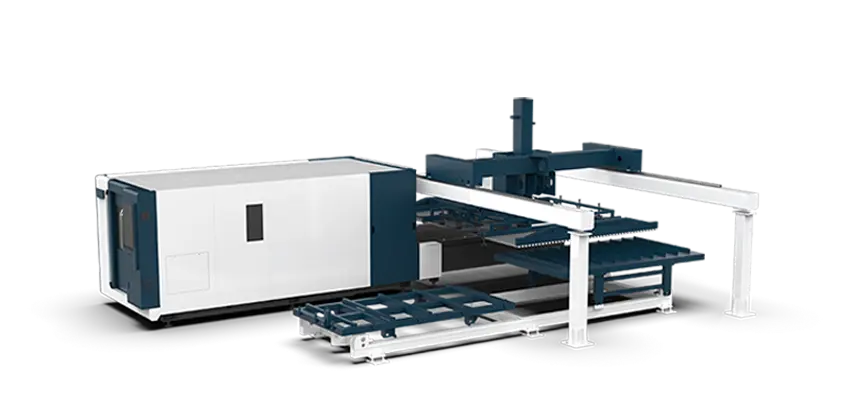
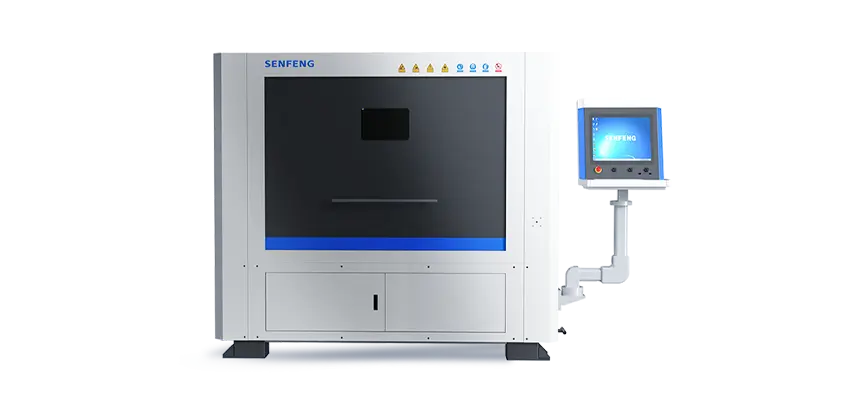
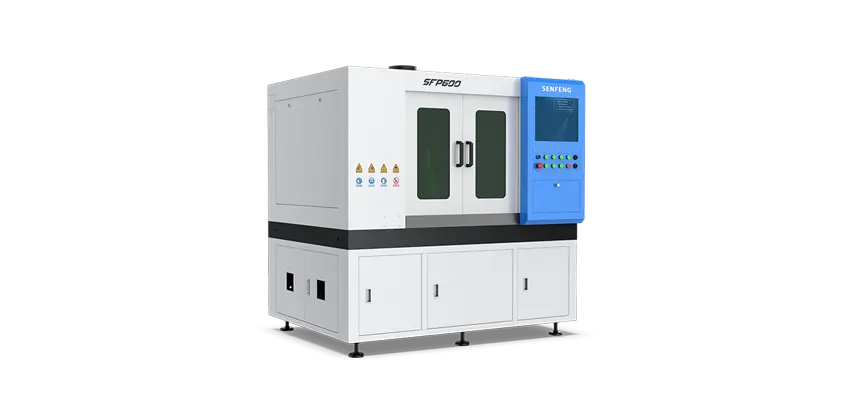
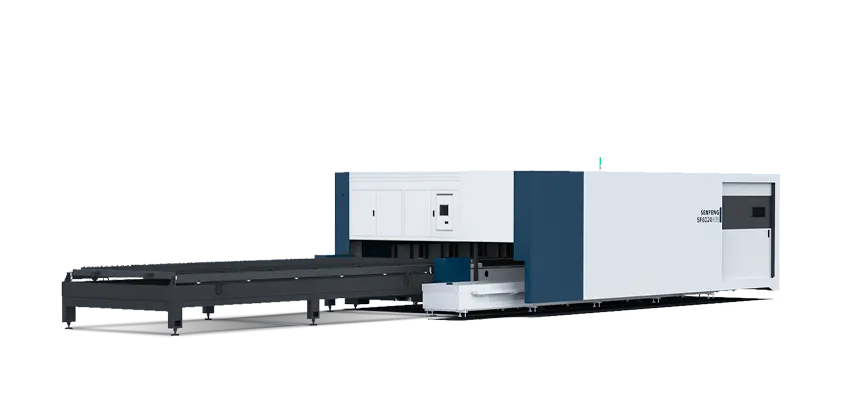
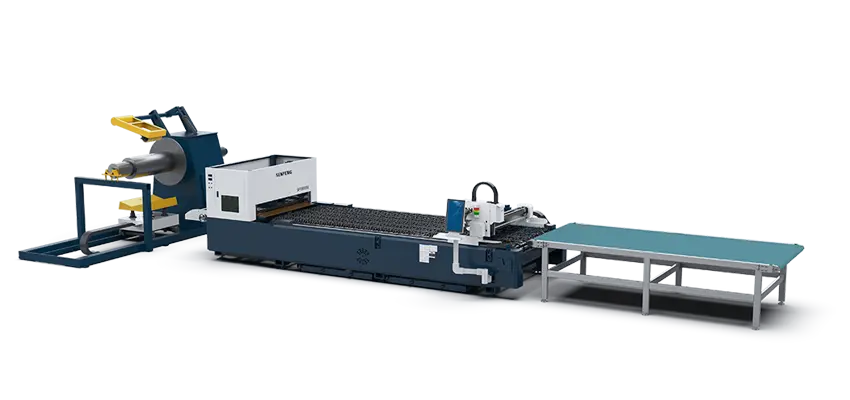
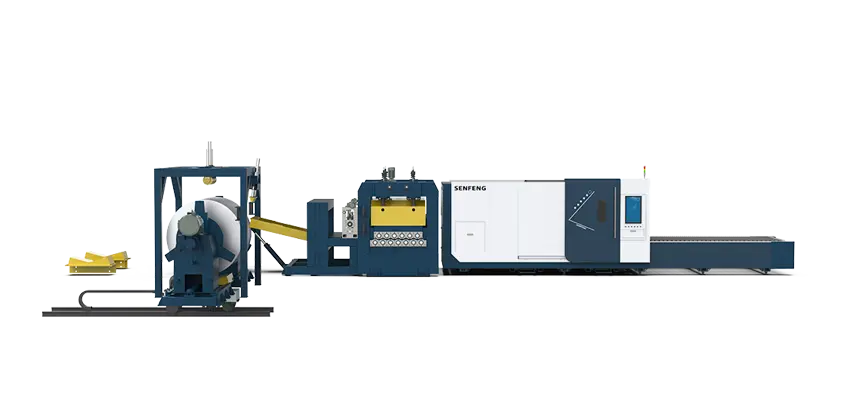
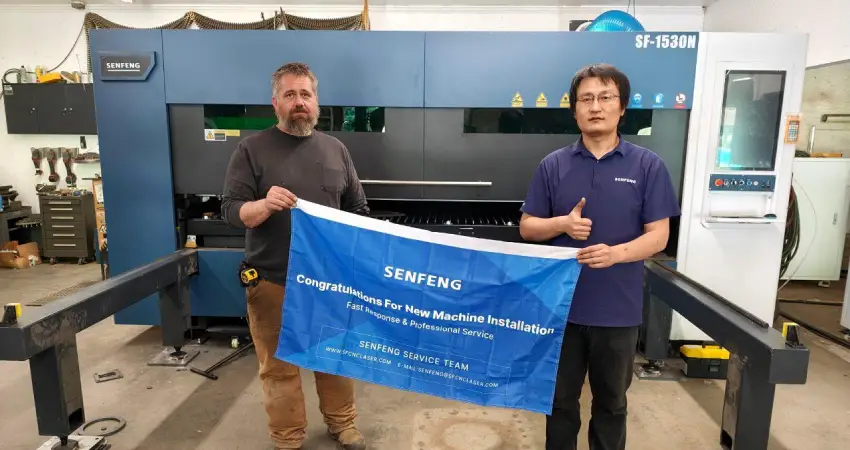
SENFENG SF1530N 12kW Fiber Laser Cutting Machine Installation and Commissioning in the USA
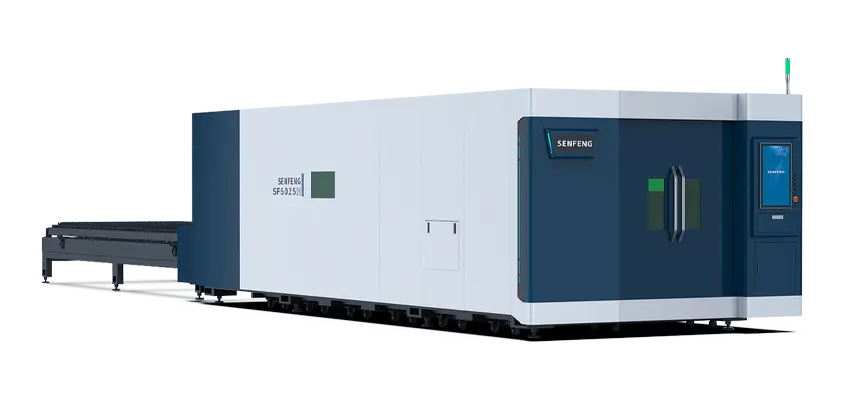
SENFENG recently completed the on-site installation, commissioning, and operator training of a SF1530N 12kW fiber laser cutting machine in the United States. The project was supported by after-sales engineer Mr. Wang, who provided full technical service throughout mechanical installation, electrical integration, system debugging, and operator training.
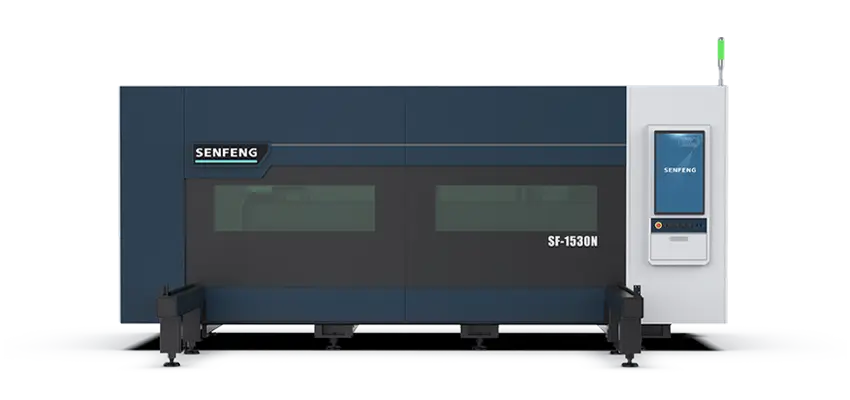
The entire project covered multi-stage work including machine positioning, auxiliary system connection, communication verification, laser commissioning, and cutting parameter optimization. After systematic setup and testing, the equipment was successfully commissioned and placed into stable operational condition.
Machine Setup and On-Site Preparation
June 8, 2026
At the beginning of the installation, the machine had already been unpacked, while most supporting accessories were still stored within the machine enclosure. The installation team first organized and removed all internal components to prepare for assembly.
Due to the compact internal structure, accessories were carefully taken out through side access openings to ensure safe handling and efficient workflow.
Key preparation tasks included:
- Machine positioning and alignment
- Base marking and leveling preparation
- Anchor point layout and foundation adjustment
- External accessory arrangement planning
Once the base positioning was completed, the mechanical structure was prepared for leveling and further integration work.
Mechanical Installation and System Wiring
After completing initial positioning, the installation moved into mechanical assembly and electrical connection.
Work included:
- Control cabinet installation and wiring integration
- Water chiller and cooling system pipeline connection
- Air supply system installation and pressure line setup
- Operator interface and display mounting
- Signal cables and electrical routing verification
All subsystems were gradually connected to ensure stable coordination between motion control, laser source, cooling system, and auxiliary units.
Auxiliary System Setup and Communication Check
June 9–10, 2026
During early power-on testing, the air supply system and communication network required structured inspection and adjustment.
Main tasks included:
- Air system inverter communication configuration verification
- Bus communication stability checking across modules
- Signal line inspection and correction
- Alarm analysis and system reset procedures
After parameter adjustment and wiring verification, communication between subsystems became stable, and the air supply system was successfully brought into continuous operation to support cutting trials.
Electrical Stability and System Commissioning
June 10–11, 2026
The system entered extended commissioning and stability testing mode.
Key procedures included:
- Power system parameter validation
- Communication signal stability optimization
- Auxiliary system restart and protection function checks
- System reboot and diagnostic review
After completing system synchronization and parameter optimization, the machine achieved stable operational status.
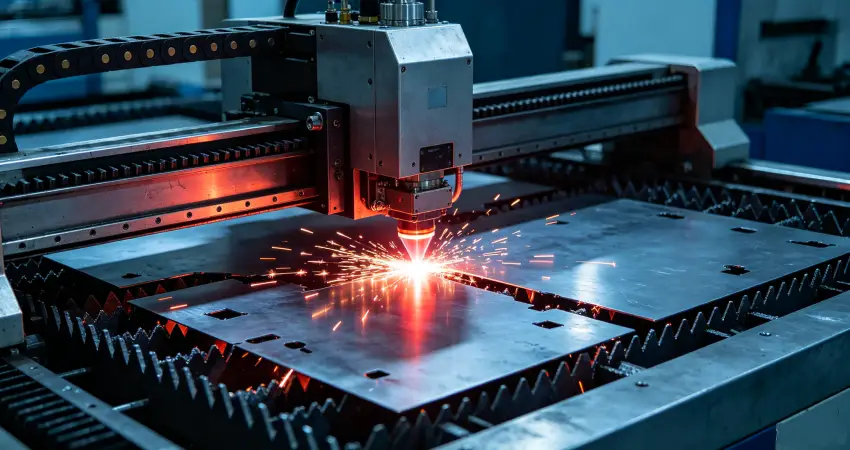
The laser cutting platform was then activated for alignment and marking tests. Initial cutting trials were conducted on carbon steel, stainless steel, and aluminum sheets, confirming stable beam output and consistent cutting performance.
Cutting Process Tuning and Optimization
June 12, 2026
With system stability confirmed, focus shifted to process optimization and parameter refinement.
Adjustments included:
- Thick carbon steel cutting parameter tuning with focus control
- Stainless steel nitrogen cutting optimization
- Aluminum sheet cutting stability improvements
- Nozzle selection and cutting head calibration
- Assist gas pressure and process refinement
Multiple material thicknesses were tested, and cutting performance was gradually optimized to ensure smooth edges, stable kerf control, and reliable piercing results.
Operator Training and Maintenance Guidance
Alongside system commissioning, structured operator training was conducted, covering both operational workflow and maintenance practices:
- Cutting software operation (file import, nesting, execution)
- Process parameter selection and adjustment
- Cutting head centering and alignment calibration
- Consumable replacement (nozzles, ceramic rings, filters)
- Routine maintenance procedures (lubrication, air system care)
- Safety guidelines and basic troubleshooting methods
Operators also participated in hands-on exercises to reinforce understanding of system operation and production workflow.
Practical Operation and Production Simulation
June 13–15, 2026
Training transitioned into independent operation practice, where operators performed real cutting tasks under guidance.
Activities included:
- Workpiece cutting practice using actual production files
- Parameter fine-tuning and adjustment exercises
- Optical center recalibration practice
- Standard workflow repetition for production readiness
During this stage, additional optimization was applied to both air cutting and nitrogen-assisted stainless steel processes, improving stability and consistency across different materials.
Final Verification and Project Completion
June 16, 2026
In the final stage, the system underwent comprehensive verification and operational confirmation.
Final tasks included:
- Reinforcement of operational procedures
- Maintenance and safety instruction review
- Independent operation validation
- Final cutting stability confirmation
After completing all system checks and ensuring consistent performance across tested processes, the SF1530N 12kW fiber laser cutting machine was officially handed over for continuous production use in stable condition.